Optimizing Frozen Poultry Facilities: An Introduction to Automatic Roll Intake
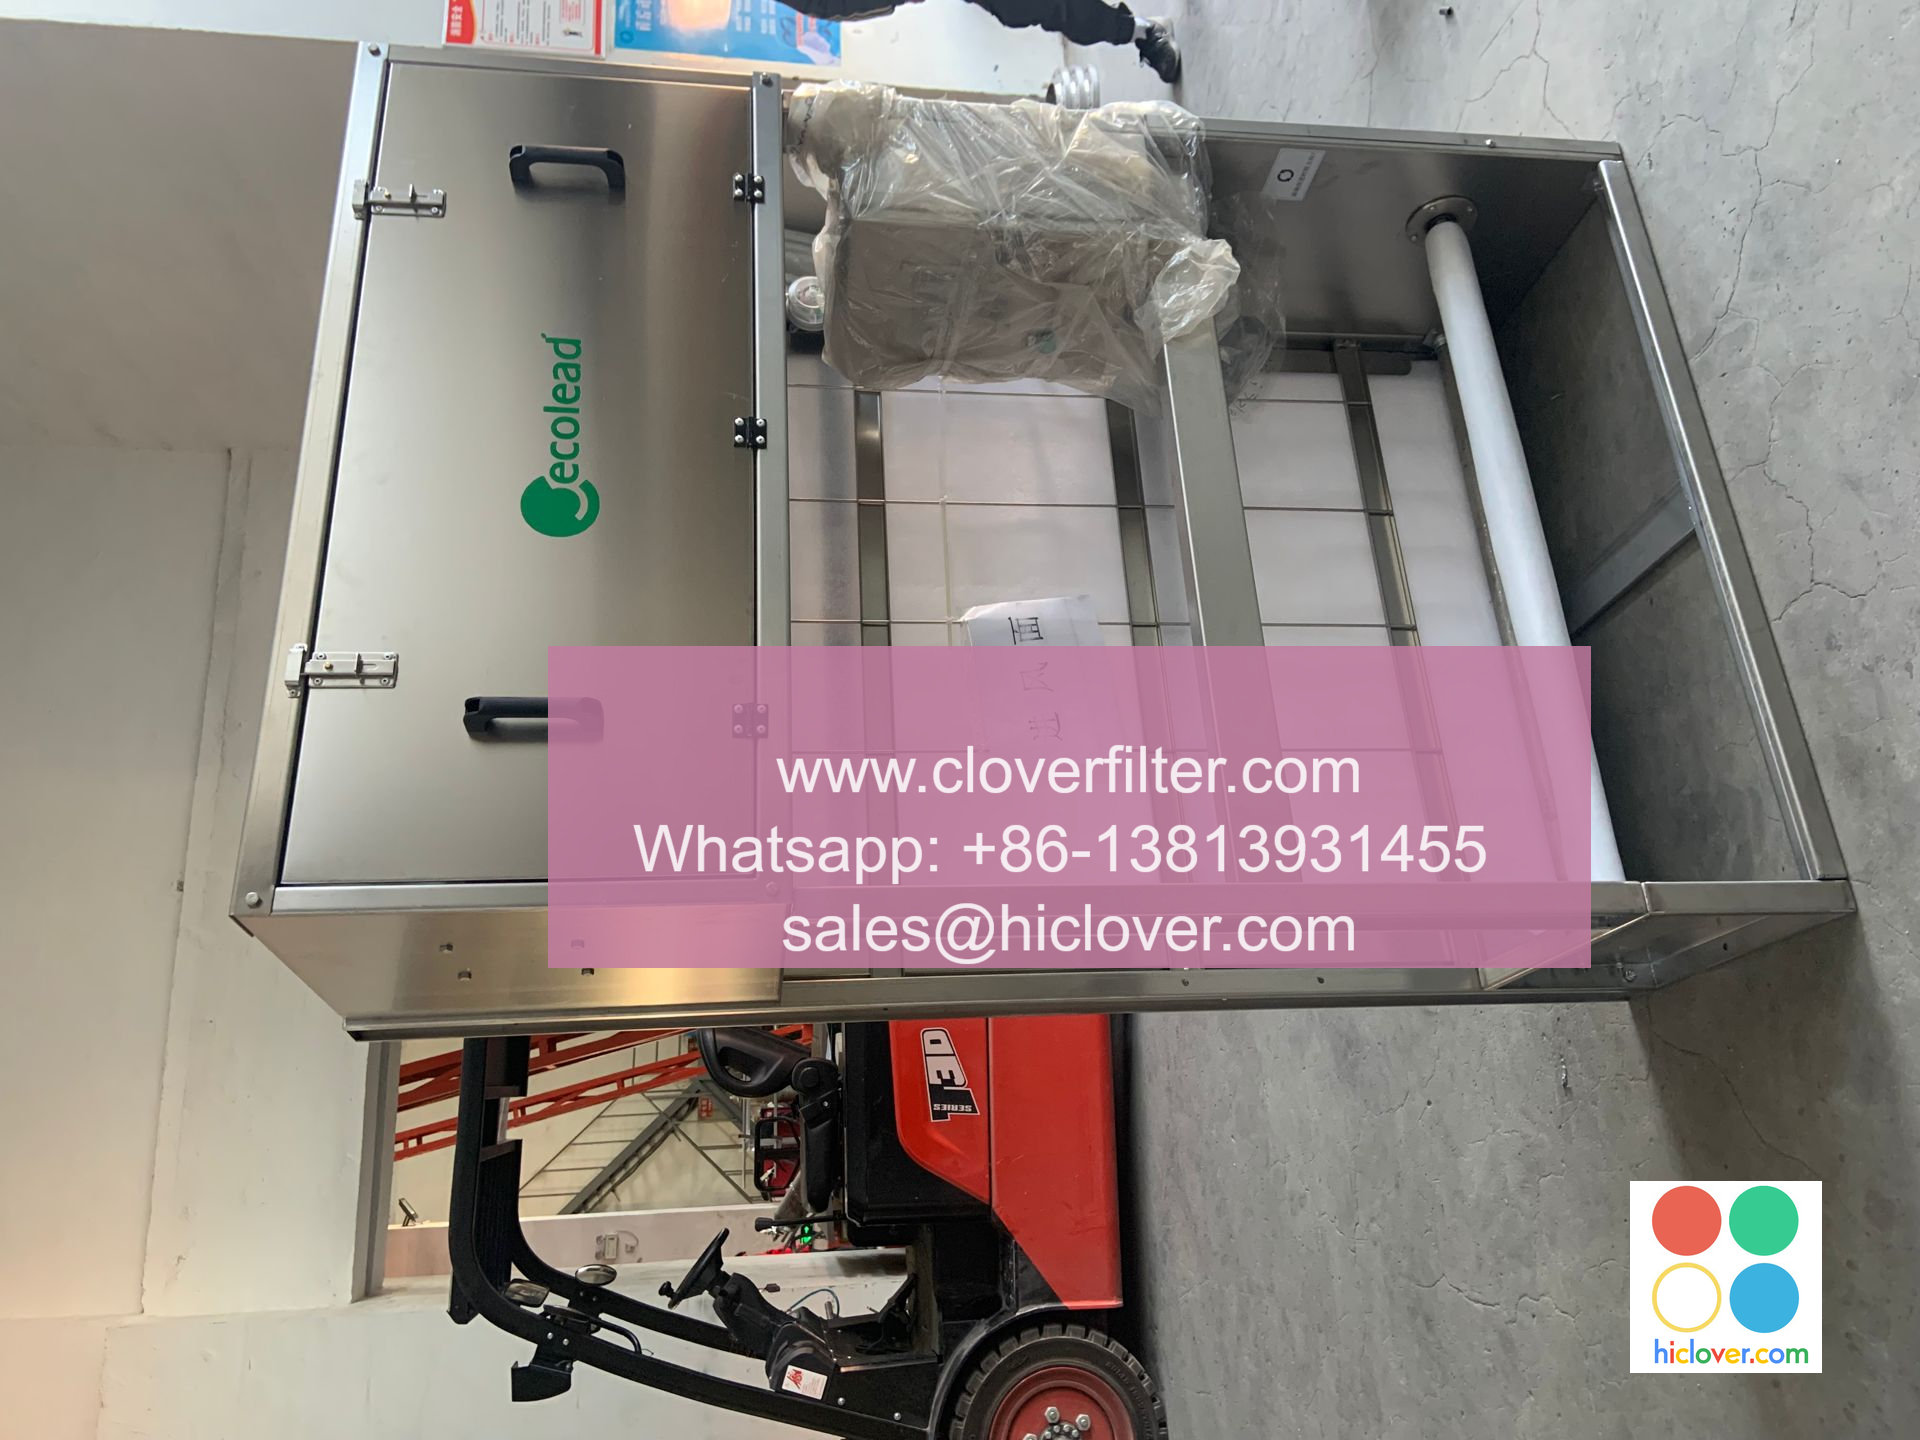
As the demand for high-quality poultry products continues to surge, the optimization of frozen poultry facilities has become increasingly crucial. One promising solution is the integration of Automatic Roll Intake, which significantly enhances both efficiency and productivity. In this article, we will explore what Automatic Roll Intake is, how it operates, and its various application areas within frozen poultry facilities.
What is Automatic Roll Intake?

Automatic Roll Intake is an advanced system designed to streamline the intake process of frozen poultry products. By utilizing automated rollers and conveyor systems, this technology minimizes manual handling and facilitates a smoother operation, which leads to reduced labor costs and increased throughput.
Key Benefits of Implementing Automatic Roll Intake
1. Improved Efficiency
Efficiency is paramount in maintaining a competitive edge in the frozen poultry market. Automatic Roll Intake allows for faster loading and unloading of products, helping facilities to keep pace with rising consumer demands.
2. Enhanced Product Safety
By minimizing manual handling, Automatic Roll Intake reduces the risk of contamination, ensuring that products remain safe for consumption. This is particularly important in the poultry industry, where safety standards are stringent.
3. Cost Reduction
The automation of the intake process not only decreases the need for a large workforce but also lowers operational costs. Energy-efficient systems can further contribute to significant savings over time.
Application Areas of Automatic Roll Intake
1. Cold Storage Facilities
Cold storage facilities can benefit immensely from Automatic Roll Intake systems. These facilities can maintain optimal temperature conditions while ensuring that the processes remain efficient and seamless, ultimately leading to better inventory management.
2. Processing Plants
In processing plants, the speed and efficiency of product handling are critical. Automatic Roll Intake can provide a continuous flow of frozen products through various processing stages, minimizing delays and maximizing productivity.
3. Distribution Centers
Distribution centers dealing in frozen poultry products demand rapid inventory turnover. Implementing Automatic Roll Intake ensures that products are swiftly received and dispatched, enhancing overall logistics management.
Conclusion
As the frozen poultry industry continues to evolve, the adoption of innovative solutions like Automatic Roll Intake will play a pivotal role in enhancing productivity and efficiency. This technology not only optimizes operations but also ensures the safety and quality of poultry products. Investing in such systems can lead to substantial long-term benefits, making it a wise choice for frozen poultry facilities aiming for future growth and sustainability.
It looks like you entered “Prompt,” but I’m not sure what you’re looking for. Could you please provide more details or specify a topic or question you’d like me to respond to?
