Case Study: Improving Production with Automatic Roll Filters in Pelletizing
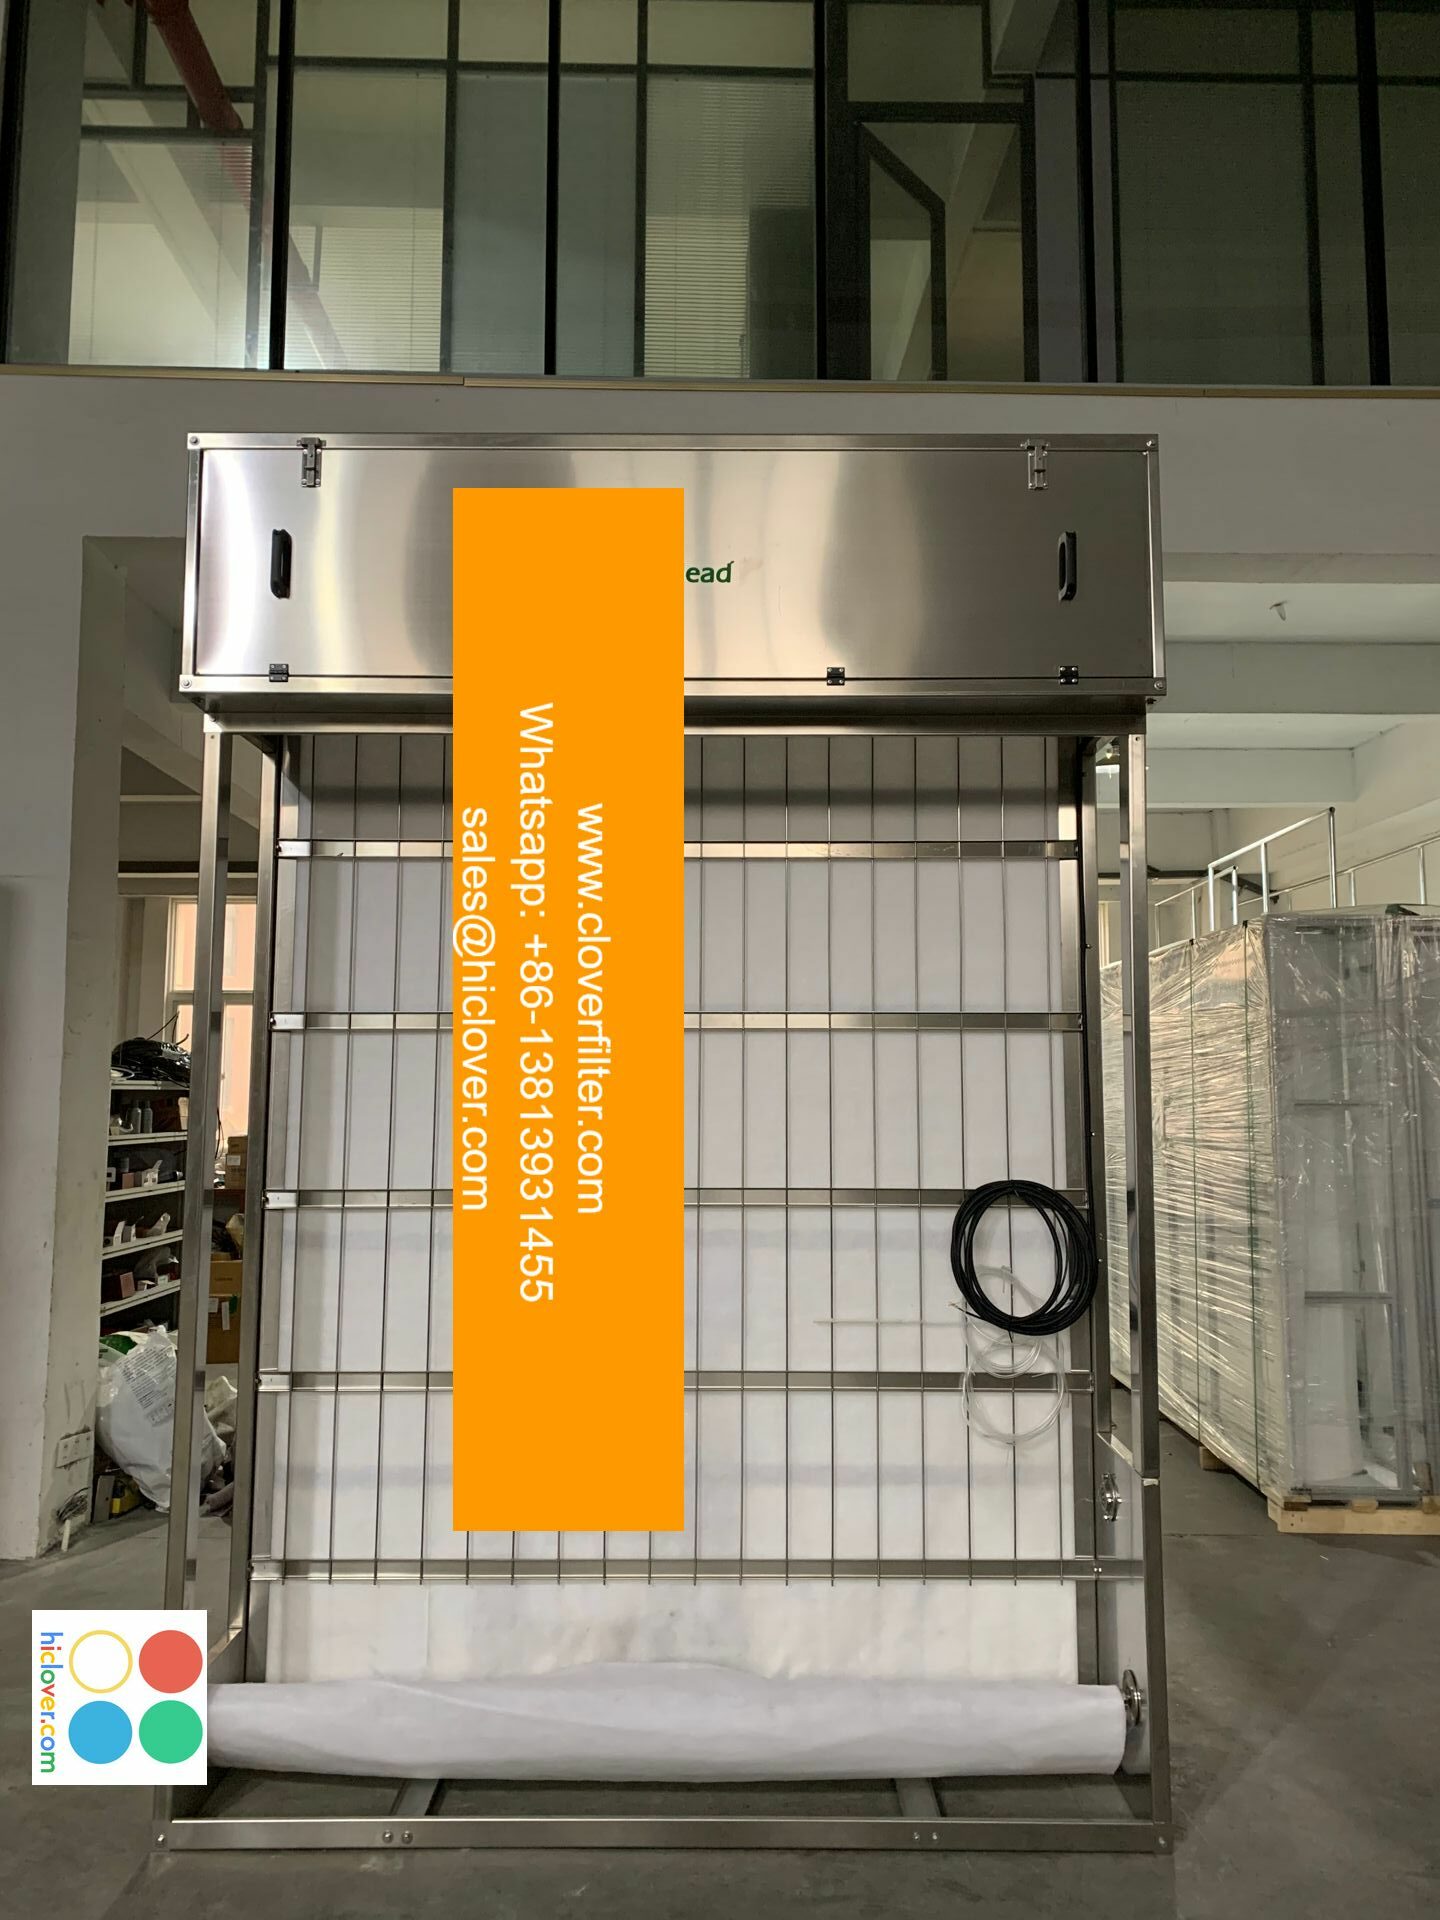
In the fast-paced world of manufacturing, enhancing production efficiency is crucial to staying competitive. One area that has seen significant innovation is the pelletizing process, particularly through the implementation of automatic roll filters. This case study explores how these filters can vastly improve production quality and reduce maintenance costs.
Understanding the Pelletizing Process

Pelletizing is essential in industries such as mining, agriculture, and plastics. It involves transforming raw materials into pellets, ensuring consistent size and quality for downstream processes. In this industry, even a minor improvement in the efficiency can lead to substantial economic benefits.
Challenges Faced in Traditional Pelletizing
Many traditional pelletizing operations experienced challenges like:
- Frequent equipment malfunctions due to excessive contamination
- High maintenance costs associated with manual cleaning and filter changes
- Inconsistent pellet quality leading to variability in product performance
- Minimizing Downtime: Automated systems decrease the need for manual intervention, allowing for continuous operation.
- Reducing Maintenance Costs: These filters require less frequent maintenance, significantly lowering operational expenses.
- Improving Product Quality: By providing consistent filtration, they help maintain uniform pellet size and integrity.
- Mining: Enhancing the extraction process by ensuring that ore particles are filtered effectively.
- Agriculture: Improving fertilizers’ quality through effective filtration of raw materials.
- Chemicals: Ensuring that various chemical compounds are produced with high purity levels.
- 30% Increase in Production Efficiency: The elimination of downtime results in higher output.
- 25% Reduction in Operational Costs: Less maintenance leads to significant savings.
- Improved Product Consistency: Higher quality pellets lead to increased customer satisfaction and market competitiveness.

The Role of Automatic Roll Filters
Automatic roll filters serve as a filtration system that removes contaminants from the pelletizing process, ensuring clean, high-quality pellets. The implementation of this technology addresses the challenges mentioned earlier by:
Application Areas of Automatic Roll Filters
The versatility of automatic roll filters extends beyond just pelletizing. They are applicable in various sectors such as:
Results and Benefits
The implementation of automatic roll filters has led to:
Conclusion
In summary, integrating automatic roll filters into the pelletizing process not only addresses serious operational challenges but also enhances overall production efficiency. As industries strive for improved productivity, embracing technologies like automatic roll filters can prove to be a game changer in achieving sustainable growth.
It seems like you just entered “Prompt.” Could you please provide more details or specify what you would like to discuss or ask about? I’m here to help!
