Nestlé Canada’s North York Facility: A Showcase for Automatic Roll Air Filters in Food Processing
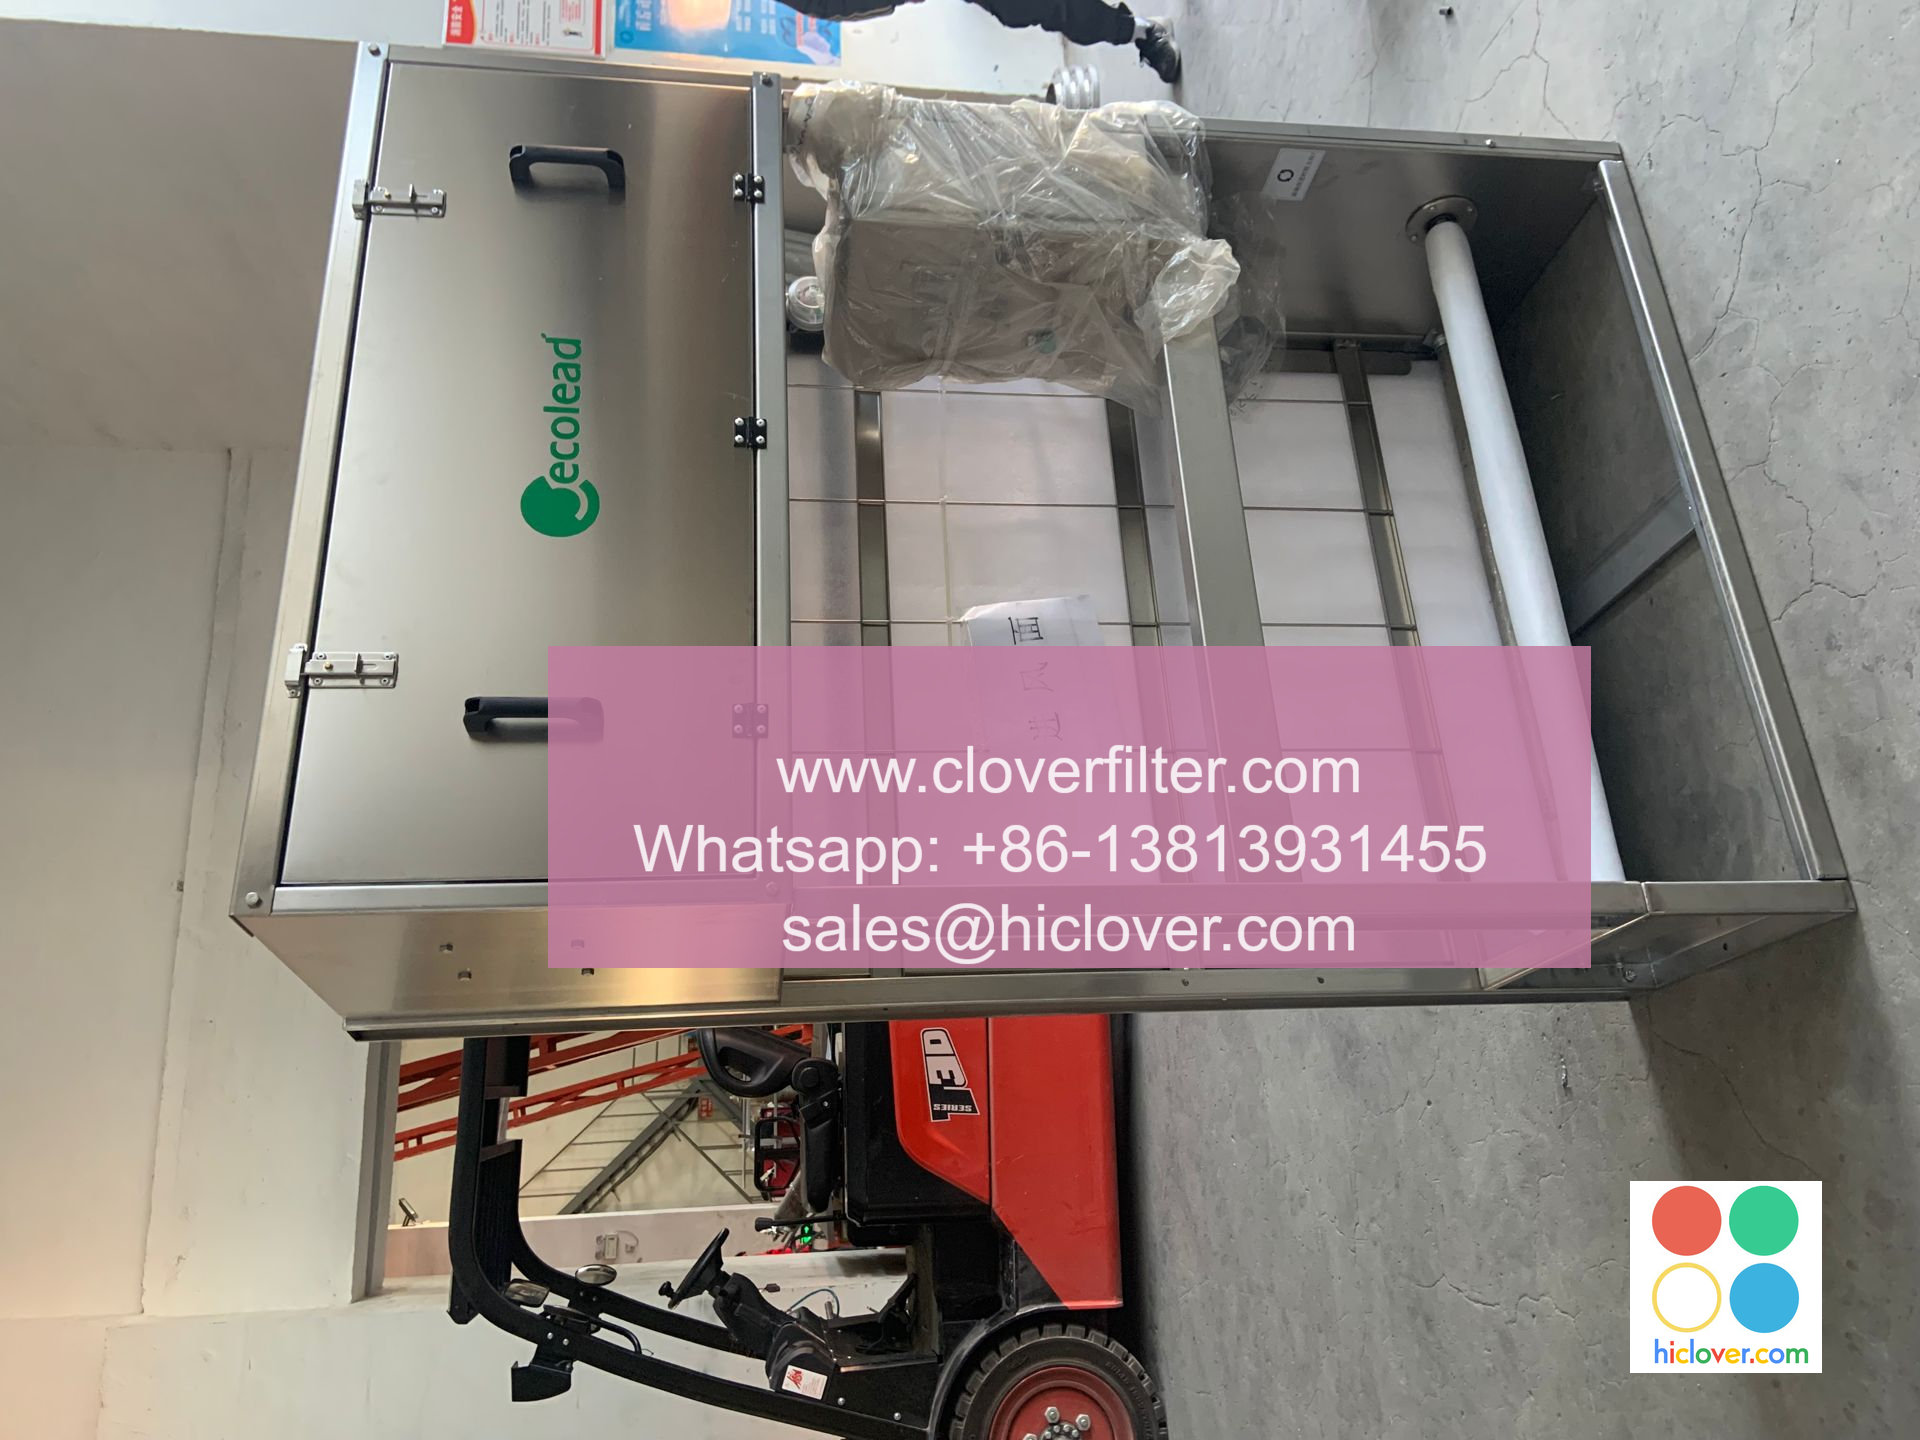
Nestlé Canada’s North York facility stands as a beacon of innovation and quality in the realm of food processing. As one of the leading food and beverage companies globally, Nestlé prioritizes hygiene, efficiency, and sustainability in its operations. A critical component of their success story is the implementation of automatic roll air filters, a technology that enhances air quality and operational efficiency across various application areas.
The Importance of Air Quality in Food Processing

In the food industry, maintaining exceptional air quality is paramount. Airborne contaminants can lead to product spoilage and compromise food safety. The North York facility utilizes automatic roll air filters to ensure that the air in production areas is continuously monitored and filtered, safeguarding the quality of products like dairy items, bottled beverages, and frozen foods.
Understanding Automatic Roll Air Filters
Automatic roll air filters are advanced filtration systems designed to capture dust, allergens, and other particulate matter in the air. Unlike traditional filters that require frequent manual replacement, these filters operate seamlessly to provide continuous air purification. At Nestlé Canada, this automation minimizes downtime and lowers maintenance costs, resulting in a more efficient production environment.
Key Applications of Automatic Roll Air Filters
1. Dairy Processing
In dairy processing, where hygiene is critical, automatic roll air filters play a vital role in preventing contamination. By ensuring clean air circulation, these filters help maintain the freshness and safety of milk, yogurt, cheese, and other dairy products manufactured at the North York facility.
2. Beverage Production
For beverage production, clear air pathways are essential to prevent the introduction of unwanted particles during bottling and packaging processes. The automatic roll air filters aid in maintaining sterile conditions, particularly in the production of soft drinks, juices, and bottled water.
3. Frozen Food Manufacturing
The demand for frozen foods has surged due to changing consumer preferences. In the frozen food aisle, air quality directly affects product integrity. Automatic roll air filters contribute to maintaining optimal air quality, thereby reducing the risk of freezer burn and preserving the quality of products like frozen vegetables and ready meals.
4. Confectionery Production
Nestlé’s confectionery products, including chocolates and sweets, require a delicate balance of environmental conditions. The integration of automatic roll air filters ensures that air contaminants do not affect ingredients or final products, guaranteeing safety and quality that consumers trust.
Sustainability and Energy Efficiency
Nestlé Canada is committed to sustainability, and the use of automatic roll air filters aligns perfectly with this mission. These modern air filtration systems are not only more effective but also energy-efficient. By reducing energy consumption associated with traditional HVAC systems, these filters contribute to the overall reduction of the facility’s carbon footprint.
Conclusion
The Nestlé Canada facility in North York showcases how cutting-edge technology, like automatic roll air filters, can drastically improve air quality and efficiency in food processing. Through various applications—from dairy to beverages and confectioneries—Nestlé maintains rigorous standards for hygiene and quality. As the food industry continues to evolve, embracing innovative solutions is key to meeting consumer demands and ensuring safety in food production.
In summary, the North York facility not only serves as a manufacturing hub but also as a model for leveraging technology to enhance operational efficiency and uphold the health standards necessary for food processing. Emphasizing the critical role of air quality, Nestlé Canada sets a high bar for the industry, reinforcing the importance of adopting advanced solutions in food manufacturing environments.
